Calibration is the invisible bridge between a glass cutting machine’s mechanical precision and the finished product’s dimensional accuracy. Even the most advanced cutting tables can produce defective parts if calibration is neglected. This article provides simple, actionable calibration tips for achieving high-accuracy glass cuts, helping you reduce material waste, improve edge quality, and extend the service life of your equipment. Whether you are a process engineer or a shop floor manager, these practices will directly impact your bottom line.
Why Calibration Matters for Glass Cutting Accuracy
Glass cutting is a process where small errors compound quickly. A misaligned bridge, worn linear guide, or incorrect blade offset can turn a nominal 1000 mm cut into a 1002 mm cut. For industries like architectural glass or precision furniture, such deviations are unacceptable. Calibration ensures that the machine’s actual movements match its programmed coordinates. It also accounts for tool wear, thermal expansion, and mechanical backlash. Without regular calibration, you are essentially trusting a machine that has drifted from its original specification.
Core Components That Require Calibration
- Linear axes: X and Y axes must be squared and have consistent scaling across the entire travel length.
- Blade holder and scoring head: The blade’s vertical position, pressure, and angle must be repeatable.
- Conveyor and table surface: Flatness and parallelism affect glass support and cutting depth consistency.
- Optional rotary or multi-blade units: Angular alignment and spacing need periodic verification.
Establish a Calibration Schedule Based on Usage
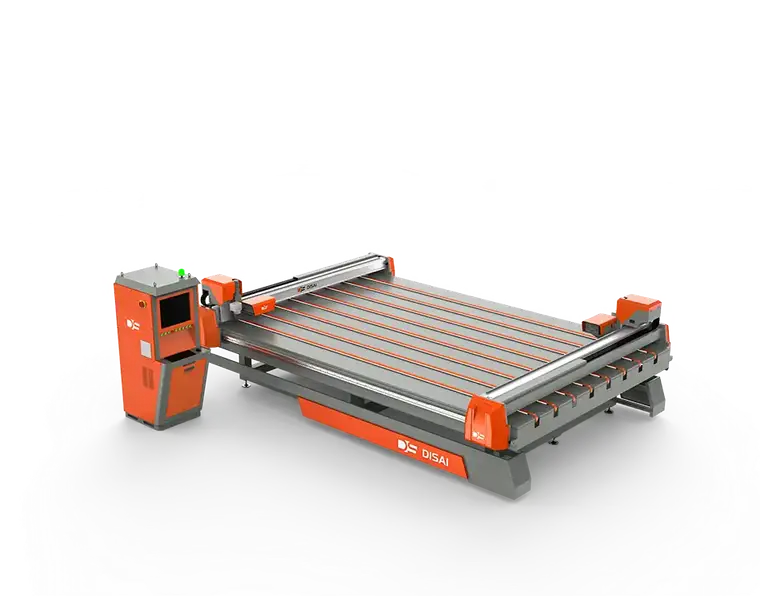
There is no universal calibration interval that fits every production environment. A machine cutting 6 mm glass continuously will lose calibration faster than one used for short runs. As a rule of thumb, verify critical parameters weekly, perform a full calibration monthly, and always recalibrate after any mechanical maintenance or impact event.
For high-accuracy glass cuts, we recommend maintaining a simple log. Record the date, operator, ambient temperature, and measured deviations. This data will help you spot trends before they become defects. If you notice a gradual increase in deviation on one axis, it may indicate a worn bearing or loose coupling—both easier to fix early.
Simple Weekly Checks for Consistent Precision
- Cut a known reference square and measure diagonals. Difference should be within 0.5 mm per meter.
- Check the zero position of the scoring head using a dial indicator on the cutting table.
- Inspect blade rotation and replace if worn. A dull blade creates pressure variations that affect cut depth.
- Clean the linear guide rails and apply proper lubrication per manufacturer specifications.
Practical Calibration Tips for Setting Blade Depth and Pressure
Blade depth and pressure are the two most sensitive parameters in glass cutting. For standard float glass, the score should penetrate about 10% to 15% of the glass thickness. However, this percentage varies with glass type and coating. Instead of relying solely on theoretical formulas, perform a simple wedge test: cut a strip, break it, and inspect the score line. A proper score is clean, uniform, and without micro-chipping along the edges.
When adjusting pressure, use the lowest value that produces a complete score. Excessive pressure causes deeper cracks and introduces residual stress, leading to unpredictable breaks. Many modern machines from manufacturers like DISAI include load sensors and digital pressure controls, but these must still be calibrated to a known reference. Use a pressure gauge or test glass to confirm that the displayed value matches the actual applied force.
How Temperature Drift Affects Calibration
Glass cutting machines operate in environments that can change temperature by several degrees between morning and afternoon. Steel expands at roughly 12 µm per meter per degree Celsius. On a 4-meter cutting table, a 5°C shift can cause 0.24 mm scaling error. For high-accuracy glass cuts, this is significant. Measure a reference length at the coldest and warmest parts of the day, then decide if temperature compensation is needed. Some controllers include thermal compensation features—use them. If not, schedule critical cuts during stable thermal periods.
Verify Cut Quality with Simple Tests
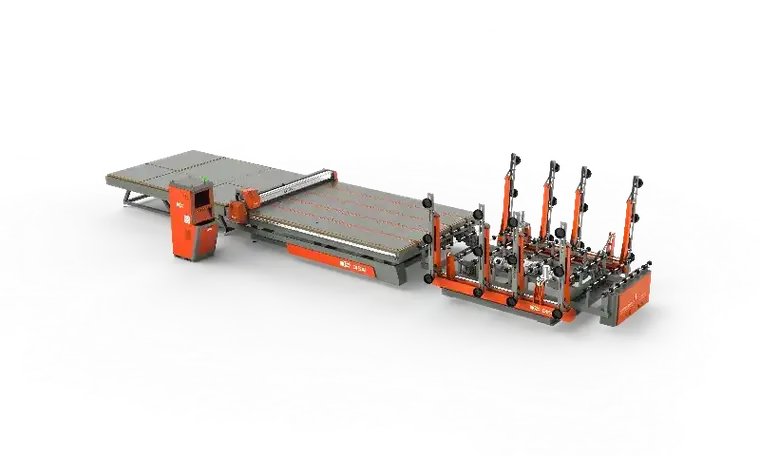
Calibration does not end with machine settings. The final proof is the cut glass itself. Use these simple tests to validate accuracy:
- Dimension check: Measure each produced piece after cooling. Record min and max values.
- Squareness test: Place a part against a calibrated square and check for gaps greater than 0.2 mm per 500 mm.
- Break consistency: If the same line breaks with different edge angles, blade alignment may be off.
- Chipping assessment: Visual chipping on the score line usually indicates excessive pressure or incorrect blade angle.
Whenever possible, automate this verification. A simple laser micrometer or camera-based edge inspection can immediately flag drift. But even manual checks, when done systematically, catch most calibration issues before they become costly rework.
Common Calibration Mistakes to Avoid
Understanding what not to do is as valuable as knowing the correct procedure. Here are mistakes we frequently see in production environments:
- Using worn reference parts: Always verify your square and gauge blocks against a known standard.
- Ignoring backlash: If you only calibrate in one direction, reverse error remains. Always approach the reference point from the same direction, or measure both directions separately.
- Calibrating on a dirty table: Glass splinters and dust change thickness readings. Clean thoroughly first.
- Forgetting to update the control parameter: You calibrated the machine, but did you save the new offset values? It happens more often than you think.
- Neglecting the breaking bar: A misaligned breaking bar can cause cut glass to break along incorrect lines, appearing as a calibration error.
Leveraging Machine Software to Simplify Calibration
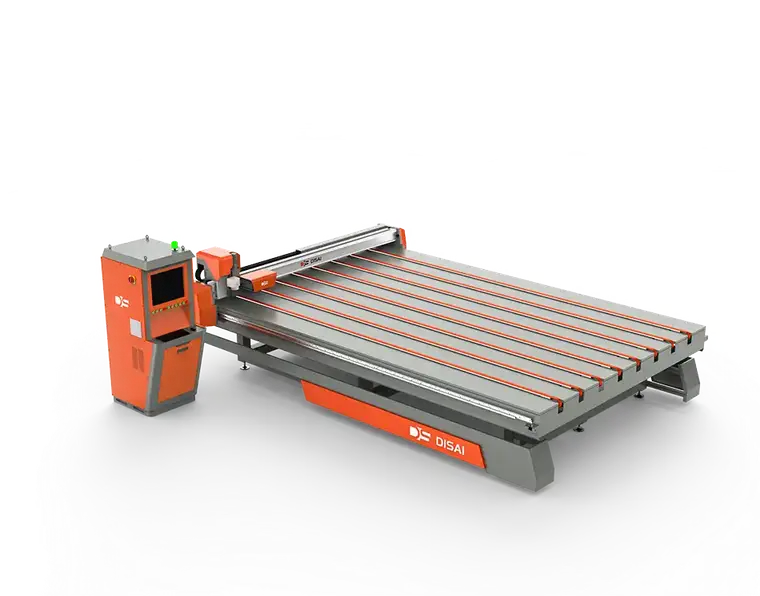
Modern CNC glass cutting machines offer built-in calibration routines that can significantly reduce manual effort. These routines often guide the operator step by step, using a touch probe or a calibrated reference tool. If your machine supports such features, use them consistently. However, remember that software calibration compensates for mechanical errors—it does not eliminate them. A loose motor coupling or a bent guide rail will eventually defeat any software offset.
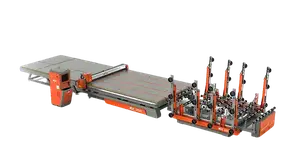
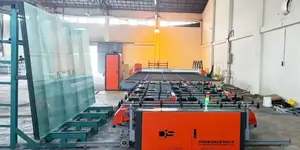
DISAI glass cutting machines, for example, come with precision-ground guide rails and high-resolution encoders that maintain mechanical accuracy over long service life. Yet even the most robust components benefit from periodic software-based calibration. Consult your machine manual for the recommended procedure, and don’t hesitate to contact the manufacturer’s technical support if you observe unexplained deviations.
Building a Culture of Precision
Calibration is not a one-time event. It is a daily discipline that requires operators, maintenance teams, and quality control to share the same goal. Train your staff to recognize warning signs like inconsistent breaking edges or increasing dimension spread. Encourage them to record unusual observations without fear of blame. A transparent root-cause approach will reveal whether the issue is mechanical, procedural, or environmental.
Finally, consider the return on investment. A structured calibration program reduces waste, improves first-pass yield, and strengthens customer trust. In a market where high-accuracy glass cuts are a competitive advantage, precision becomes your business identity.
By following these simple calibration tips, you can keep your cutting process stable, your glass edges clean, and your production schedule on time. Start with the basics, document your results, and refine your routine as your machine ages. Consistent calibration is the simplest way to achieve the accuracy your customers expect.